A ceramic tiles manufacturer can pass a sample review and still create site problems if approvals, production batches, packing labels, shipment lots, and installation zones are managed as separate activities. Project contractors need one connected release system. A zone-release plan links the approved sample to a defined production batch, assigns that batch to a specific area, verifies its packing evidence, and prevents installers from opening material that has not cleared the agreed hold points.
This approach is useful for hotels, retail interiors, residential towers, transport hubs, and facade packages where thousands of tiles must look and perform like one coordinated system. It is especially valuable for relief and 3D surfaces, custom colors, mixed formats, phased deliveries, or projects with tight replacement windows.

Why a Good Sample Is Not Yet Project Control
An approved sample defines intent, but it does not automatically control mass production. The sample may come from a pilot run, a laboratory board, or a carefully selected carton. The project order may be produced over several shifts, kilns, glazing runs, molds, or packing dates. Without traceability, the team cannot prove which material matches the approval or where a changed condition entered the process.
The first task is to convert the sample into a release record. Record the product code, nominal format, thickness, surface, edge, color reference, relief profile, acceptable visual range, caliber, test basis, packing method, and approved date. Add photographs taken under agreed lighting and retain matching physical pieces with the factory, buyer, inspector, and site team.
For applicable technical requirements, buyers can consult the ISO 13006 ceramic tile classification requirements as an authority source, then name the relevant standard and test method in the purchase specification. A general statement such as “ISO quality” is not a measurable acceptance criterion. The release record should state what is tested, the acceptance limit, the sampling method, and the document that proves the result.
Build One Control Map from Product to Installation Zone
A practical zone-release plan begins with the project drawings. Break the tile package into areas that can be produced, inspected, packed, delivered, and installed without losing identity. A zone might be one hotel floor, one lobby elevation, a group of bathrooms, a facade grid, or a retail unit.
Each zone record should include:
- drawing reference and installation location;
- product, format, surface, color, pattern, and quantity;
- approved sample or mockup reference;
- planned production batch and shade or caliber group;
- inspection and documentation status;
- carton and pallet identification;
- shipment, arrival, storage, and installation status;
- reserve quantity and replacement-stock location.
The map should be simple enough for the factory packer and the site storekeeper to use. A sophisticated schedule that never reaches the carton label has little operational value. Use the same zone code across the purchase order, production plan, inspection report, packing list, pallet mark, delivery note, storage map, and installer release sheet.
Establish Hold Points Before Production Starts
Hold points stop the process until defined evidence is accepted. Agree them before the order is released, not after a problem appears. Typical hold points include technical submittal approval, pilot production, full-scale mockup, first-off production, mid-run comparison, pre-packing inspection, pre-shipment review, site-arrival check, and installation-area release.
The MagiTiles factory and tile quality-control overview helps contractors frame discussions about raw materials, forming, firing, surface processing, sorting, and packing. Translate that capability discussion into project-specific evidence. For example, the first-off release may require a multi-piece panel compared with the retained standard, dimensional readings from a defined sample, profile checks for textured pieces, and photographs showing carton identification.
Set decision owners and response times. If the architect must approve the visual panel, state how quickly the review will occur and what happens if it is delayed. If the factory quality team may release routine batches within an approved range, define the range and the records it must keep. Unclear authority is a common cause of production waiting, rushed shipment, or unauthorized substitution.
Control Shade, Caliber, Relief, and Pattern Separately
Tiles that share a product code can still vary in ways that matter at installation. Shade affects visual continuity. Caliber affects joint alignment. Warpage influences lippage. Relief depth changes shadow and edge transitions. Printed or veined surfaces need a pattern distribution rule. Each variable should have a control method and an escalation boundary.
A 3d ceramic tiles manufacturer should demonstrate the surface at panel scale under frontal and grazing light. A single piece cannot show repeated shadows, module rhythm, corner conditions, or mold wear. For customized reliefs, retain a master profile or approved mold reference and compare early, middle, and late production panels.
Do not confuse architectural wall-tile controls with another product category. An alumina ceramic tiles manufacturer may prioritize composition, abrasion, and industrial lining performance. A brick ceramic tiles manufacturer search may refer to brick-look tiles, ceramic slips, or a different wall system. Clarify application, substrate, exposure, and test evidence before importing terminology or limits from a different category.
Release Production in Lots That Match the Site Plan
The safest production lot is not always the largest possible run. It is the largest lot that can maintain the approved range while remaining traceable and useful to the construction schedule. Coordinate lot size with floor sequences, elevation boundaries, storage capacity, and inspection timing.
At the end of each controlled lot, assemble a random panel from several cartons rather than selecting only attractive pieces from the line. Compare it with the retained approval under the agreed lighting. Record shade, caliber, dimensions, surface, relief, edge quality, and packaging observations. If the result approaches a boundary, investigate before more material is produced.
This is where supplier location should become a logistics question rather than a shortcut for quality. A ceramic tiles manufacturer in Morbi or a ceramic tiles manufacturer in Bikaner may offer useful production clusters and export routes, but geography does not prove traceability. Evaluate the actual plant, equipment, process control, project evidence, communication, and ability to reproduce the accepted range.
Make Zone Packing Part of the Quality Plan
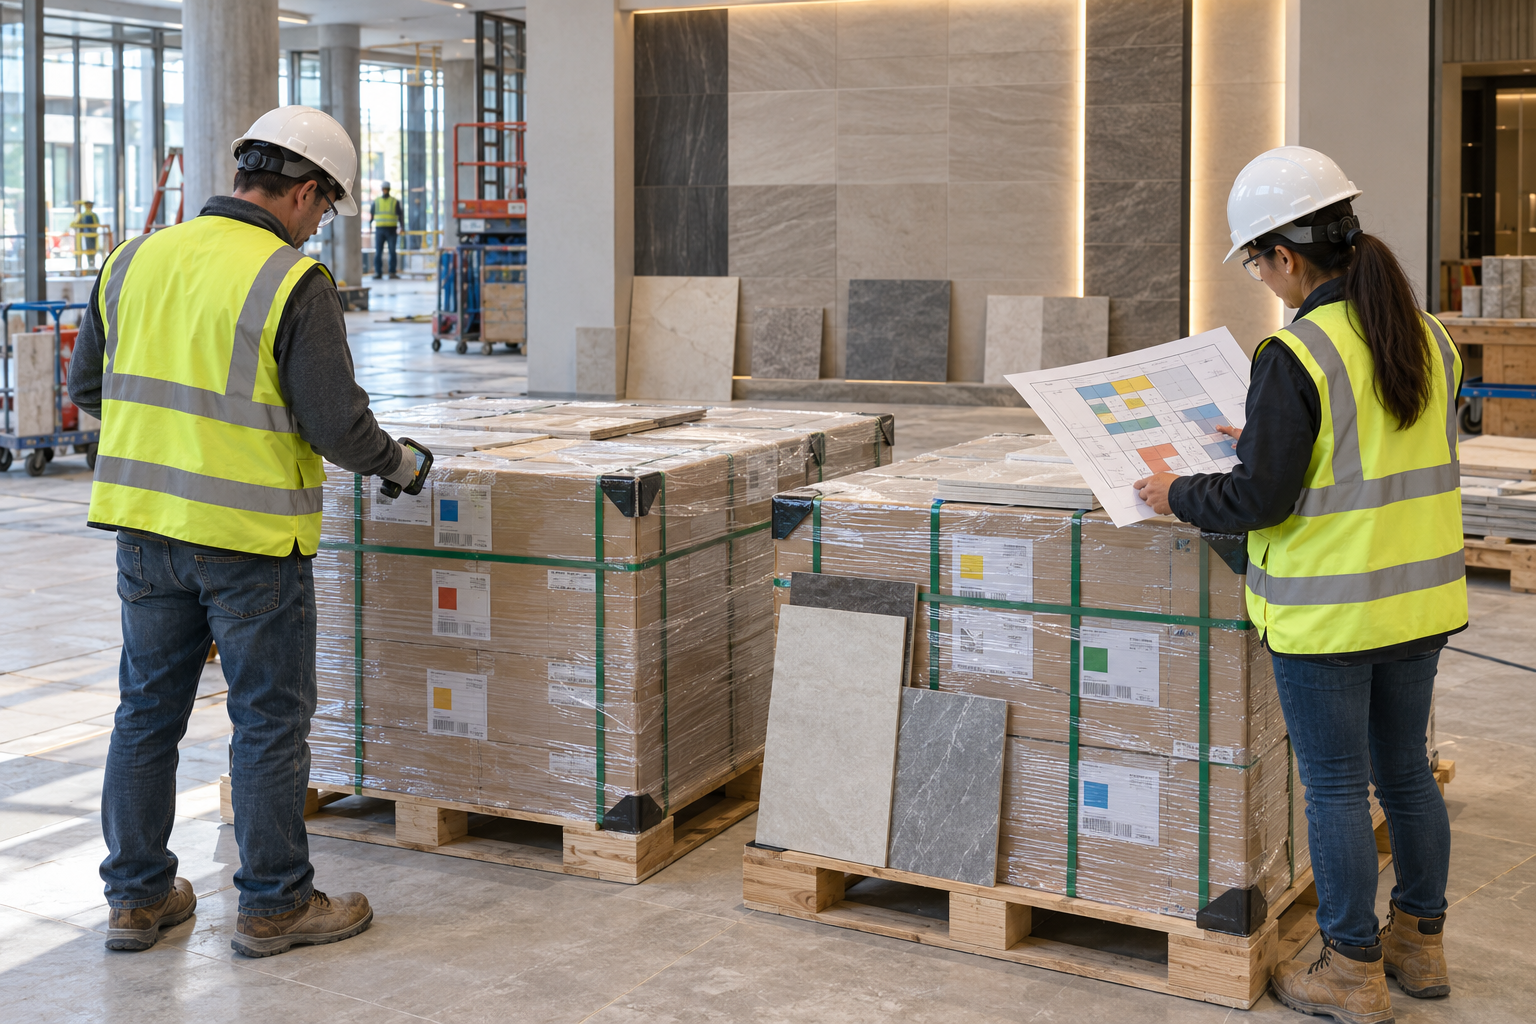
Packing is not merely protection; it is the bridge between production identity and installation location. Every carton should carry the project product code, batch, shade or caliber group where relevant, quantity, and zone. Each pallet should show its zone, pallet number, carton count, gross weight, and handling instructions. The packing list should reconcile with both the production release and the project zone map.
For relief tiles, specify separators, face protection, corner protection, carton strength, stacking direction, pallet coverage, moisture protection, and maximum stack height. For mixed-format layouts, decide whether components will be packed as installation sets or as separately counted items. The right answer depends on breakage risk, installer workflow, and replacement needs.
Reserve stock must keep its identity. Do not create one unallocated pool that mixes batches from several zones. Assign compatible spares to the area they can repair, and record when stock is transferred. That discipline prevents an early shortage from consuming the only matching pieces needed for a later floor.
Verify Delivery Before Material Enters the Installation Flow
Site teams often discover discrepancies only after pallets have been moved, wrapping removed, or cartons distributed. Add an arrival gate. Check pallet count, visible damage, moisture exposure, labels, zone allocation, and packing-list reconciliation before accepting material into storage.
Store pallets by zone and batch, not simply by product family. Protect them from water, contamination, impact, and unauthorized issue. Photograph pallet marks and storage positions. When the installation area is ready, release only the compatible material for that zone and retain representative pieces for later comparison.
Review MagiTiles ceramic tile project cases when defining the handoff between design intent, product selection, mockup, logistics, and installed result. Comparable projects are most useful when they help the buyer ask about real viewing distances, lighting, module transitions, corner details, and delivery constraints—not when they serve only as decorative references.
Connect the Release Plan to Installation Acceptance
The final release is an installation decision. Confirm substrate condition, datum, joint width, setting method, pattern direction, movement joints, trims, corners, cleaning, protection, and lighting before production material is fixed. Use a signed site benchmark so new crews and later phases have the same reference.
The responsibility matrix should distinguish product acceptance from installation workmanship and design suitability. The ceramic tiles manufacturer supplies evidence for the product and agreed customization. The contractor controls storage, setting materials, workmanship, and protection. The designer or responsible professional confirms the assembly and local requirements. Shared checkpoints make these responsibilities visible without turning every issue into a dispute.
If an exception appears, quarantine the affected cartons and identify their batch and zone. Do not spread questionable material across several areas. Record the observation, compare it with the retained approval, determine the scope, and agree a disposition: accept, sort, rework, replace, or hold. The traceability system should allow the team to locate every related pallet quickly.
Turn the Plan into a Project-Ready Inquiry
The buying funnel should become more specific at each step. First, define the tile direction: application, format, body, finish, color, relief, performance basis, and expected quantity. Use MagiTiles tile sourcing insights to structure early technical questions and compare options against the project rather than against a generic catalog.
Second, confirm factory and OEM/ODM capability for custom molds, color matching, pattern development, private labels, carton artwork, zone marks, pallet plans, retained samples, test records, and replacement continuity. Third, submit the drawings, zone schedule, mockup requirement, inspection hold points, destination, delivery sequence, site constraints, and decision owners in one inquiry package.
Finally, use the MagiTiles tile sourcing insights to share that package with the supplier team. A clear request allows the manufacturer to price the required controls, not just the tile. It also lets the contractor compare suppliers on evidence, responsibility, and schedule readiness.
A reliable ceramic tiles manufacturer should be able to show how an approved sample becomes a released batch, a labeled pallet, a verified delivery, and an accepted installed zone. When every handoff carries the same identity and evidence, project control no longer depends on memory or last-minute sorting. The result is a more predictable finish, faster decisions, and a cleaner route from product selection through OEM/ODM coordination to site completion.