A ceramic tiles manufacturer may quote a competitive price and provide a datasheet in which every value appears acceptable. That still does not tell a project contractor what the finished wall will look like across hundreds of square metres. Specifications usually describe nominal values, averages, or permissible limits. An installed surface reveals the range: shade movement, relief depth, edge definition, caliber, joint rhythm, reflectance, and the way adjacent pieces respond to light.
That difference is especially important when evaluating a 3d ceramic tiles manufacturer. Small variations that are harmless on an individual piece can become visually dominant when repeated across a lobby, retail wall, hotel corridor, or facade. Buyers therefore need to approve and control a production range—not just a perfect sample or an average test result.
Why Price and Nominal Specs Miss the Installed Result
Price comparisons work only when suppliers are offering the same scope and control level. One quotation may include shade sorting, caliber segregation, panel inspection, protective separators, zone labels, retained samples, and replacement stock. Another may cover only standard production and ordinary export packing. The unit prices are not comparable until those differences are made visible.
Datasheets can create the same false equivalence. Two products may share nominal size, thickness, water absorption, and strength while differing in production-range control. For architectural tiles, the buyer must understand both the technical compliance envelope and the visual acceptance envelope.
The International Organization for Standardization provides an authoritative framework for international standards, but a project specification should identify the applicable standard, test method, product identity, acceptance limit, and responsible laboratory. “ISO quality” by itself is not a measurable purchase requirement. Standards support the decision; they do not replace a project-specific control sample and inspection plan.
Define the Approved Range Before Mass Production
An approved range is a documented set of acceptable outcomes. It should show the centre of the target and the permitted boundaries. For a tile package, that can include:
- colour and tone variation under agreed lighting;
- gloss or reflectance range;
- relief depth and profile sharpness;
- dimensions, squareness, thickness, and warpage;
- edge quality and acceptable minor imperfections;
- print, vein, or pattern distribution;
- grout-joint assumptions and module alignment;
- carton, shade, caliber, and batch identification.
The most useful approval set is not one hand-selected tile. It is a multi-piece panel drawn from a representative pilot run. The project team should record product codes, measured values, photographs, lighting conditions, sample dates, and signatures or digital approvals. Matching sets should remain with the manufacturer, buyer, inspector, and site team.
This approach turns aesthetic language into an operational reference. “Warm grey,” “subtle relief,” or “consistent surface” can mean different things to different people. A retained panel and written range allow production and inspection teams to make the same decision later.
Build a Full-Scale Mockup Around Real Viewing Conditions
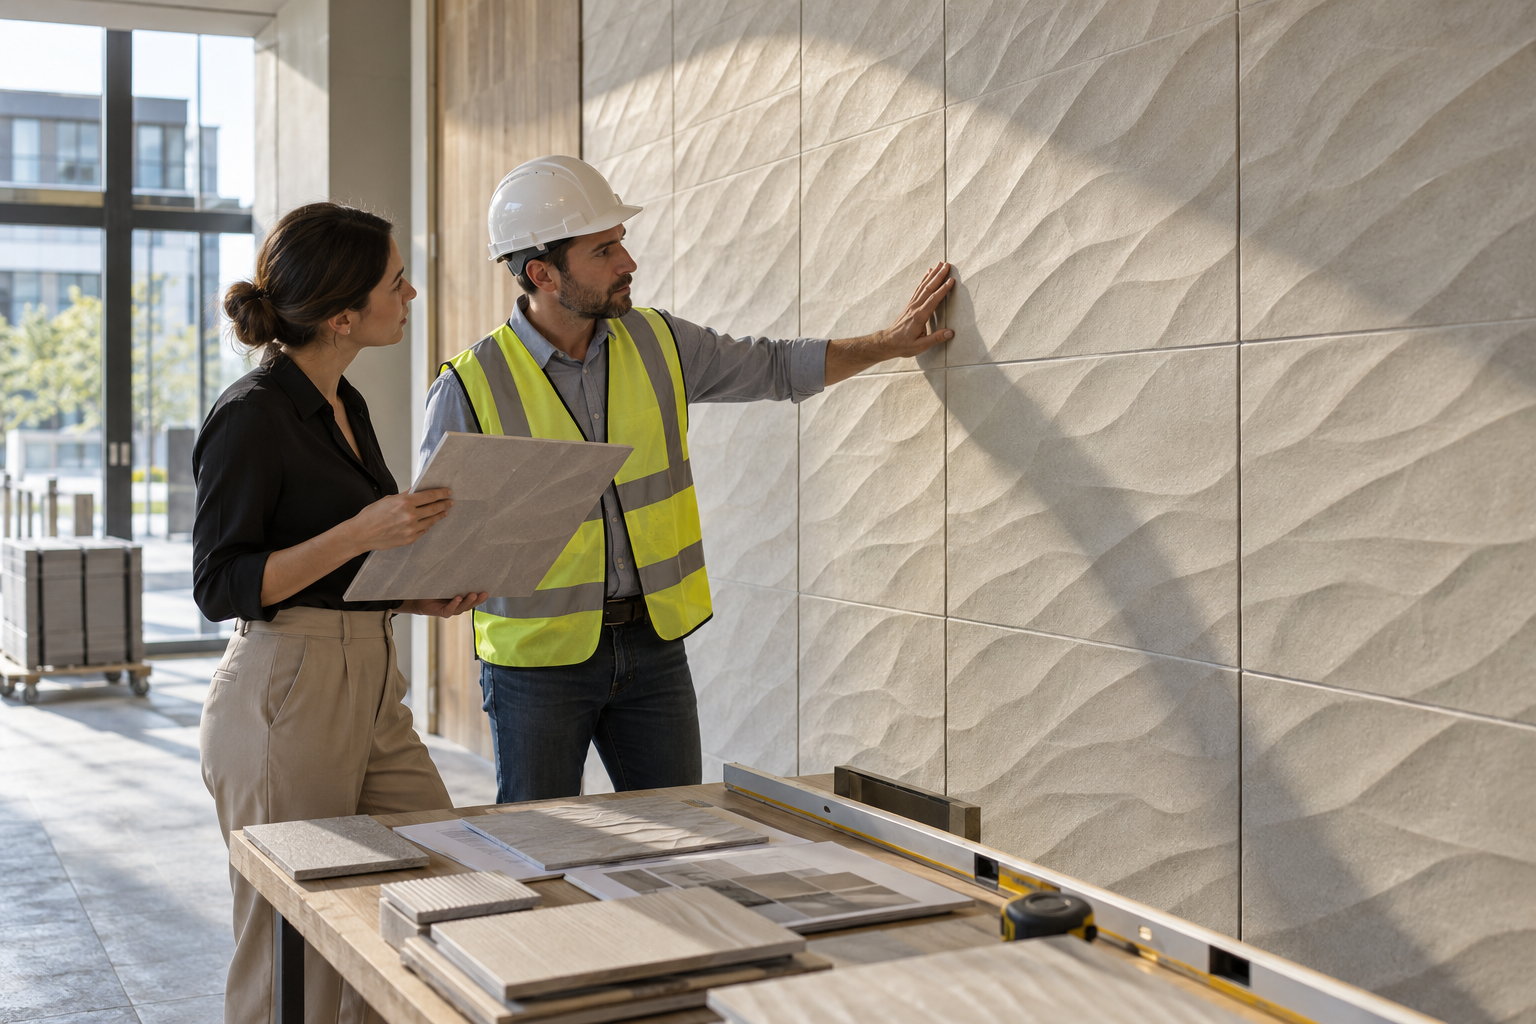
A tabletop sample cannot reproduce the installation interface. A full-scale mockup should use the intended substrate, setting method, joint width, pattern direction, corner details, trim conditions, and lighting geometry. It should be large enough to reveal repetition and cumulative alignment.
For 3D tiles, use both general illumination and grazing light. Shadows can magnify small profile or joint differences. Review the wall from the expected approach distance as well as close range. If the project includes daylight, spotlights, wall washers, or changing colour temperature, assess the mockup under those conditions before approving the production range.
The review should separate four decisions:
- Product acceptance: Is the tile itself within the agreed visual and dimensional range?
- Layout acceptance: Does the module repeat, direction, and joint rhythm support the design?
- Installation acceptance: Are the substrate, adhesive coverage, alignment, and cutting method workable?
- Lighting acceptance: Does the specified light reveal an effect the owner and architect will accept?
This separation prevents the ceramic tiles manufacturer from being held responsible for an installation or lighting issue, while also preventing product variation from being dismissed as a site problem.
Convert the Mockup into Measurable Production Controls
Once the mockup is approved, translate it into checkpoints. The MagiTiles factory and ceramic tile quality-control overview provides a practical basis for discussing raw-material control, forming, firing, surface processing, sorting, and packing evidence.
The production control plan should identify what is checked, how often, by whom, with which tool or reference, and what happens when the result approaches a boundary. For visual characteristics, specify viewing distance, light source, panel size, and comparison sample. For dimensional characteristics, record the measuring method and sampling frequency. For customized reliefs, include profile gauges, master molds, or agreed comparison points where appropriate.
Do not rely only on final inspection. If a firing or surface-process shift appears after the full order is completed, sorting and replacement can consume the schedule. Early pilot panels and in-process checks give the factory a chance to correct the process before the variation spreads.
Control Shade, Caliber, and Relief as Separate Variables
Shade and caliber are often printed together on a carton, but they create different site risks. Shade affects visual continuity. Caliber affects joint alignment and installation productivity. Relief depth affects both appearance and how neighboring modules meet. Each variable needs its own acceptance logic.

Before shipment, require a pallet and carton map that connects product code, production batch, shade group, caliber group, quantity, and installation zone. Avoid mixing incompatible groups within one elevation or room unless the approved layout intentionally blends them. If blending is required, document the method and provide installers with representative pieces from all groups before work begins.
A staged project also needs allocation rules. Material for later floors or phases should not be consumed to solve an early shortage without checking the effect on batch continuity. Reserve replacement and attic stock by compatible group, and state how long retained production samples will be kept.
Inspect the Range, Not Only Defect Counts
A conventional inspection can confirm quantity, obvious defects, packing, and selected dimensions. It may still miss whether the accepted visual range has drifted. Add panel assembly to the inspection scope. Randomly select pieces from several cartons and pallets, arrange them in the intended orientation, and compare the result with the retained approved panel.
Inspection photographs should capture the overall panel, oblique light, joints, labels, measurements, cartons, pallets, and any boundary examples. Attractive close-ups alone are not evidence of batch control. Review MagiTiles ceramic tile project cases to frame questions about real viewing distance, module layout, transitions, and site conditions before finalizing the inspection brief.
The same discipline helps buyers avoid category confusion. An alumina ceramic tiles manufacturer may be controlling composition and wear performance for industrial linings, while an architectural supplier focuses on surface appearance and modular installation. A brick ceramic tiles manufacturer search may describe brick-look wall tiles, ceramic slips, or a different construction system. Clarify the application and required evidence before treating these offers as comparable.
Add the Installation Interface to the Purchase Package
Many tile disputes occur at the boundary between product and installation. Include the following in the pre-order review:
- required substrate flatness and moisture condition;
- proposed adhesive and coverage method;
- minimum practical joint width;
- pattern direction and starting datum;
- inside and outside corner treatment;
- movement-joint responsibilities;
- cutting, drilling, cleaning, and protection method;
- mockup hold point and sign-off authority;
- criteria for stopping work and escalating variation.
The manufacturer should provide accurate product information and samples. The installer should verify site conditions and workmanship. The responsible design and engineering professionals should confirm system suitability and local requirements. A clear responsibility matrix is more useful than expecting one party to guarantee the entire assembly without controlling it.
Compare Total Installed Cost with an Evidence Matrix
Replace the simple price table with an evidence matrix. Compare bidders across product fit, approved-range definition, pilot capability, test documentation, batch traceability, panel inspection, packing design, installation support, schedule credibility, corrective action, and replacement continuity.
For each claim, request evidence: a sample, record, drawing, report, photograph, packing specification, or written procedure. Then price the likely consequences of missing controls—sorting labour, mockup repetition, delayed approvals, damaged-profile replacement, mixed-batch installation, rework, and schedule disruption. A slightly higher tile price can produce a lower installed cost when it removes uncertainty from the field.
Location should be treated in the same practical way. A ceramic tiles manufacturer in Morbi or a ceramic tiles manufacturer in Bikaner may offer cluster advantages, product specialization, or logistics options, but geography does not prove project control. Score the actual factory, process, evidence, communication, and fit for the specified application.
Move from Product Direction to OEM/ODM and a Project Inquiry
The sourcing funnel should become more specific at every step. First, define the product direction: application, format, body, surface, relief, colour, quantity, and performance basis. Second, review factory capability and comparable project evidence. Third, define OEM/ODM needs such as custom molds, colour matching, private labels, carton artwork, pallet marks, zone packing, test documents, and retained samples.
Finally, submit a project-ready inquiry containing drawings, finish references, target range, quantities, destination, schedule, mockup requirement, inspection hold points, packing plan, and decision owners. The MagiTiles tile sourcing insights can help a contractor turn early design intent into a structured technical and commercial request.
Price and specifications remain necessary, but they describe only part of the buying decision. A reliable ceramic tiles manufacturer should demonstrate how the approved range will be created, measured, separated into traceable batches, protected in transit, and reproduced at installation scale. When the project controls the range—not merely the average—the finished surface has a much better chance of matching the approved design.