A ceramic tiles manufacturer can produce material that meets an approved specification and still leave a contractor with a difficult installation if batch identity, packing sequence and site allocation are not controlled. The practical answer is a batch-to-zone release plan: a documented path connecting the approved sample to production evidence, pallet labels, delivery zones and installation acceptance.
This method gives the buyer more than a pre-shipment inspection report. It creates traceability for each decision, helps prevent mixed shades from reaching one elevation and makes it easier to isolate a problem without holding the entire project. It is especially useful when several tile formats, finishes or production lots must arrive in phases.
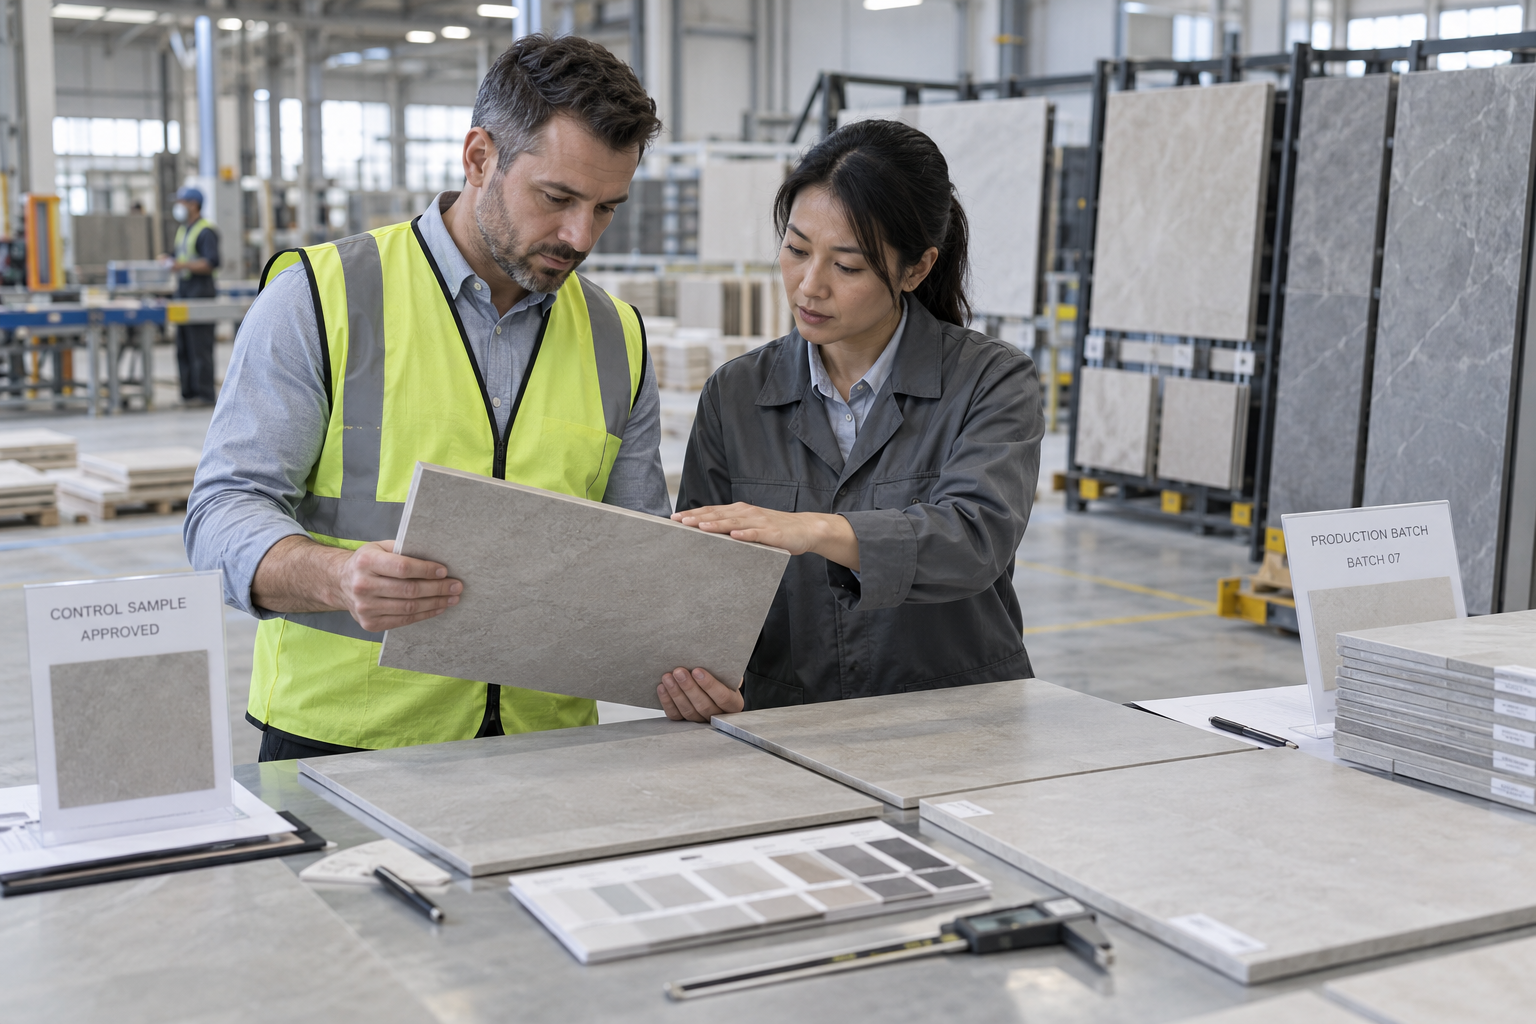
Original AI-generated editorial image illustrating a factory inspection workflow; it is not a photograph of a completed MagiTiles project.
Start With a Control Sample That Can Be Rechecked
The approved sample should be a physical reference, not only a photograph or email confirmation. Record its product code, nominal and work size, finish, shade reference, caliber, edge treatment and approval date. If the project has an architect-approved mockup, connect that record to the purchasing specification so the factory, contractor and installer are evaluating the same reference.
Ask how the supplier protects and identifies the retained sample. A loose tile without a revision number can become ambiguous after several design changes. The project file should distinguish the initial sales sample, the final approved sample and any later approved production-range board.
The MagiTiles factory overview for ceramic tile sourcing can help contractors frame questions about production and quality-control capability. For the actual order, those questions still need product-specific answers, agreed tolerances and dated evidence.
Convert the Specification Into Measurable Release Checks
A useful specification tells the inspector what to measure and what decision follows. Build a release sheet that covers at least:
- Product code, finish and intended installation zone.
- Actual dimensions, thickness, warpage and edge condition.
- Visual range for shade, surface pattern and gloss where applicable.
- Quantity by lot, carton and pallet.
- Packaging protection, carton markings and pallet identification.
- Required test reports, declarations and approved deviations.
- Inspection sample size and acceptance authority.
Do not copy a generic tolerance table into the purchase order without checking its relevance to the selected product and destination. Instead, state the applicable project standard, the measurement method and who may approve an exception. The International Organization for Standardization is an appropriate starting point for understanding standards governance; buyers should identify the exact product and test standards required by their contract, market and application.
For an alumina ceramic tiles manufacturer inquiry, engineering properties and intended industrial use may require a different verification plan from architectural wall or floor tiles. The shared lesson is to convert performance language into evidence that can be reviewed before shipment.
Freeze the Zone Schedule Before Production Release
Create a zone schedule from the latest quantity takeoff. Each line should identify the building, floor, room or elevation; product code; finish; estimated installed quantity; cutting allowance; reserve quantity; and required delivery sequence. Use stable zone codes that can appear on production records, cartons and site receiving documents.
This schedule prevents a common error: ordering the correct total quantity while overlooking where each batch will be installed. A lobby elevation should not be forced to share an uncontrolled mix of production lots simply because the total carton count is correct.
For a 3d ceramic tiles manufacturer, add pattern orientation, module sequence, corner treatment and lighting direction to the zone record. Relief surfaces can show noticeable variation when pieces rotate or when grazing light emphasizes a joint. A zone-specific mockup makes the acceptance decision repeatable.
Review relevant ceramic tile project cases and installation contexts when preparing the brief. Use them to identify questions about scale, transitions and coordination, then validate the final solution through the project’s own sample and mockup process.
Link Production Lots to the Approved Range
Before full packing, compare production samples with the retained control sample and any agreed range board. Record the lot or kiln reference, inspection date, measured results and decision. If natural or designed variation is expected, show the acceptable range across several pieces instead of approving one unusually uniform tile.
The decision should be one of three clear outcomes: accepted, accepted with a documented restriction, or rejected for correction. A comment such as “looks close” is difficult to enforce later. If a lot is limited to a secondary zone, write that restriction into the allocation schedule before cartons are labeled.
Supplier geography does not replace this evidence. Search phrases such as ceramic tiles manufacturer in Morbi or ceramic tiles manufacturer in Bikaner can help a buyer discover sourcing regions, but location alone does not demonstrate batch control, packaging quality or project coordination. Compare suppliers through the same approval and release records.

Original AI-generated editorial image illustrating site batch verification; it is not a photograph of a completed MagiTiles project.
Make Carton and Pallet Labels Serve the Site Team
Factory labels should be readable by the people receiving and installing the material. At minimum, show the product code, size, shade or lot identifier, quantity and zone code. Pallet labels should summarize their carton contents and remain visible after loading.
Where one pallet contains more than one zone, use a packing list that identifies the position and quantity of each group. Better still, avoid mixed pallets when the project sequence and container utilization allow. The small freight saving from mixed packing can be lost through site sorting, accidental distribution or delayed installation.
For a brick ceramic tiles manufacturer program, also identify pattern, corner and special-piece quantities separately. Field pieces can be plentiful while a missing corner type holds an entire elevation. Tie special pieces to the same revision and zone schedule as the main tile.
Inspect the Shipment as a System
A pre-shipment review should reconcile product evidence, quantity evidence and logistics evidence. Check that:
- production samples match the approved reference or documented range;
- inspection results match the purchase specification;
- carton counts roll up to pallet and order totals;
- shade or lot identifiers match the zone allocation;
- labels correspond to the packing list;
- protective packing is suitable for the tile format and transport route;
- replacement and reserve material is clearly identified;
- photographs show the inspected material, labels and loading condition.
Do not treat a passed visual inspection as permission to ignore documentation gaps. If labels cannot connect a carton to the inspected lot, the site team may lose the benefit of the factory review as soon as the container is unloaded.
The MagiTiles tile sourcing insights for project buyers provide further checkpoints for supplier evaluation, sampling and delivery coordination. Use those checkpoints to build an order-specific inspection brief rather than relying on a generic checklist alone.
Add a Receiving Gate Before Installation
Site receiving is the final link in the chain. Record container or vehicle condition, pallet count, visible damage and label legibility before moving material into storage. Compare received quantities with the packing list and place each pallet in its assigned zone or a clearly mapped holding area.
Open a controlled number of cartons from each lot and compare them with the site reference under representative lighting. This is not a substitute for factory inspection; it confirms that the identified material arrived and that no obvious transit or allocation problem is being passed to installers.
Define who can release material for installation. If a shade mismatch, damage pattern or label discrepancy is found, quarantine the affected lot and document it before pieces are distributed. A small, well-recorded hold is easier to resolve than removing installed work later.
Build the Inquiry Package Around Decisions, Not Adjectives
When approaching a ceramic tiles manufacturer, send an inquiry package that allows the supplier to respond with evidence. Include drawings, room or elevation schedules, target formats and finishes, quantity by zone, expected standards, sample requirements, packaging constraints, delivery phases and the decision timetable.
Ask the supplier to return:
- product and production-route confirmation;
- proposed tolerances and test evidence;
- sample and mockup sequence;
- shade and lot control method;
- packaging and label examples;
- inspection milestones;
- delivery plan and reserve-stock recommendation;
- OEM or ODM scope for colors, surfaces, formats or packaging.
This creates the full funnel from article research to product and factory evidence, then to project references, customization review and a decision-ready request. Contractors can contact MagiTiles with the project schedule and tile brief to discuss product options, OEM/ODM requirements, sampling and coordinated delivery.
A Practical Release Sequence
The strongest project-control process is simple enough for every party to follow:
- Freeze the specification and zone schedule.
- Approve a traceable physical sample or mockup.
- Confirm production-lot evidence against the approved range.
- Assign accepted lots to installation zones.
- Label cartons and pallets with matching identifiers.
- Reconcile inspection, packing and loading records.
- Verify the same identifiers at site receiving.
- Release each zone only after the receiving check passes.
This sequence does not eliminate variation or every delivery issue. It makes variation visible, assigns decisions and reduces the area affected when a discrepancy occurs. That is the real value of project control: the contractor can move from an approved sample to an installed result without losing the identity of the material along the way.